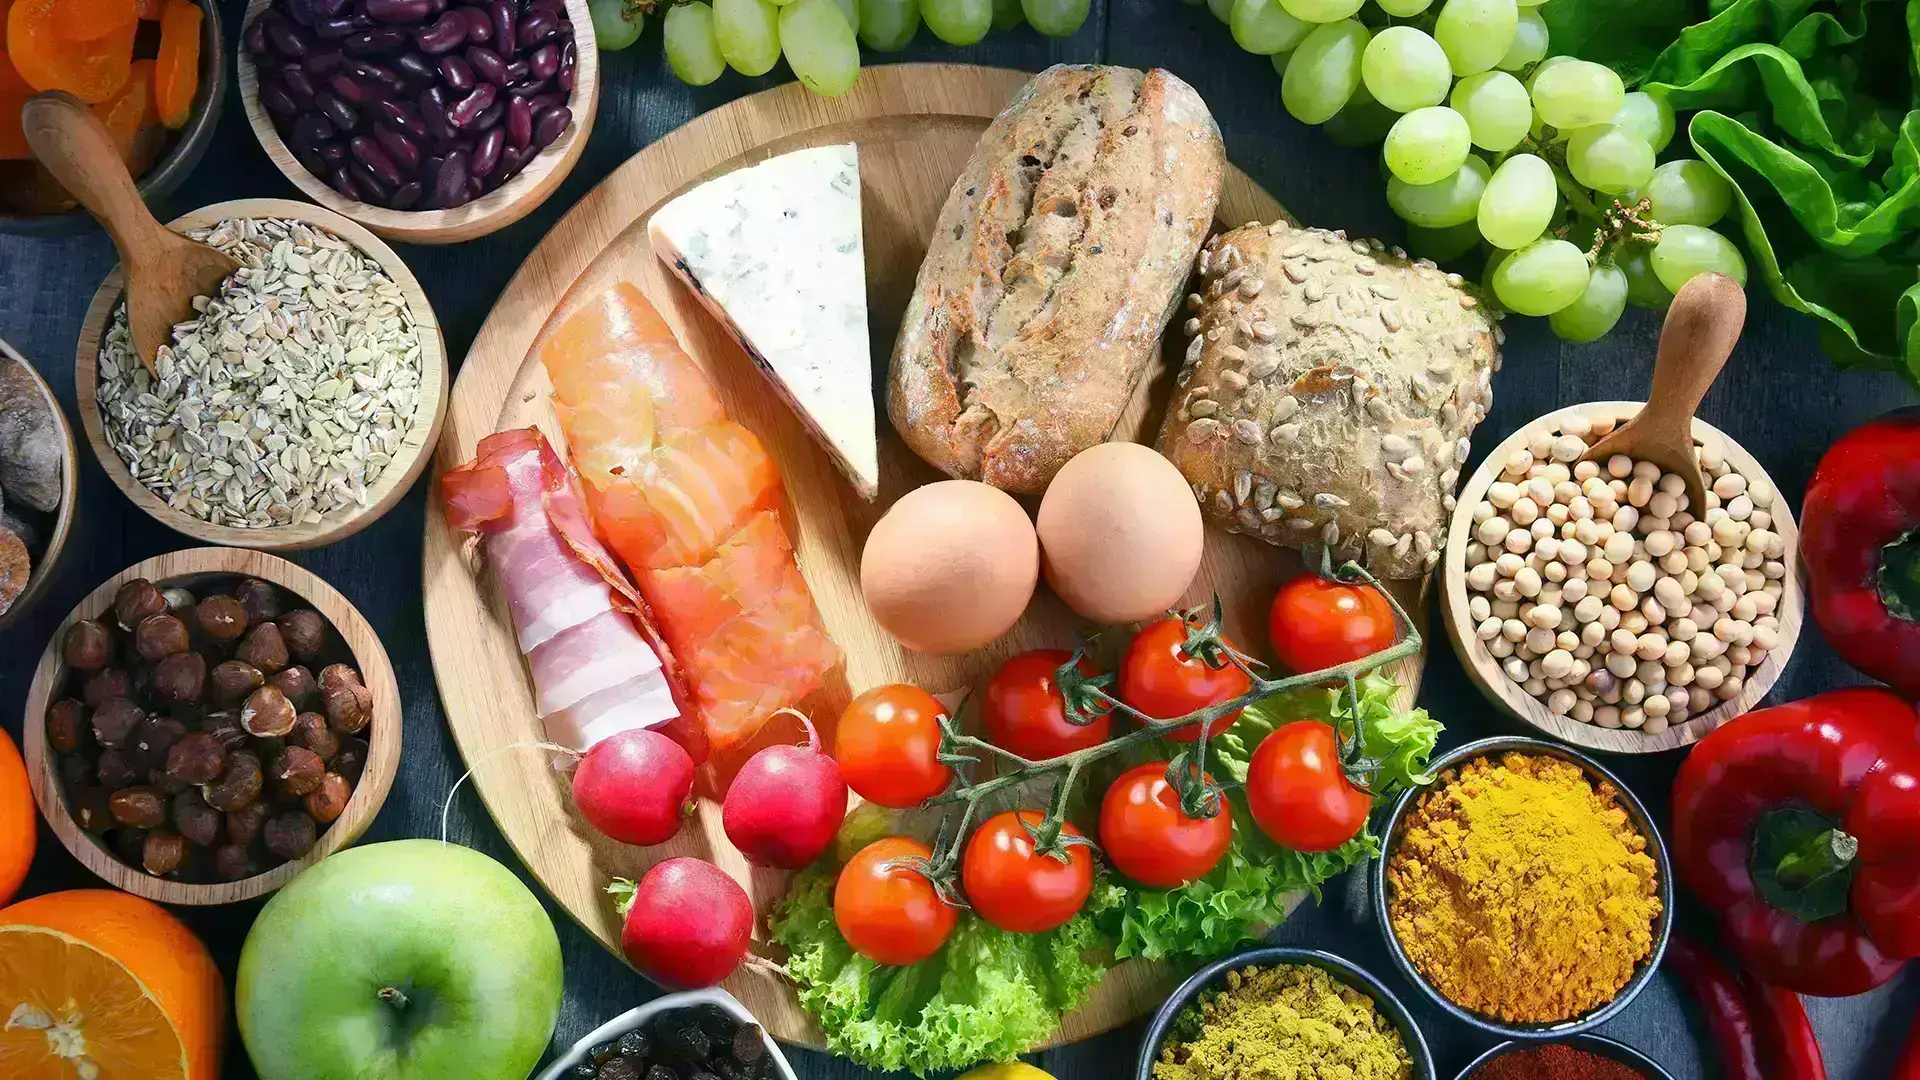
Packaging line automation for food & beverages
Turnkey automation solutions for the entire process, from bulk material handling through to high-performance, consumer-ready packaging.
Snacks
Optimize your throughput with high-performance automation designed for gentle product handling and the flexibility to rapidly switch between snack formats.
Confectionery
Maintain the integrity of delicate confectionery items with reliable systems that offer superior flexibility for varied seasonal formats.
Meats & proteins
Enhance your facility’s hygiene and reliability with integrated case packing and palletizing solutions tailored for strict food safety standards.
Dairy products
Maximize your line's flexibility and accessibility with sanitary automation designed to handle diverse dairy containers and retail formats.
Bakery
Drive production efficiency and format agility with complete end-of-line systems that help preserve the freshness and presentation of your bakery goods.
Flours & starches
Simplify your flour and starch production with specialized dust-control automation that ensures weight accuracy and high-volume consistency.
Nuts & edible seeds
Secure your competitive edge with integrated sorting, bagging, and palletizing solutions that handle high-value seeds with high precision.
Sugar
Streamline your sugar packaging, from bulk to industrial formats and more, with accurate, clean, and safe automation that minimizes product loss.
Coffee
Help preserve the freshness your coffee blends with specialized handling and filling technology, including innovative jute bag solutions.
Pasta, beans & rice
Achieve high-capacity, reliable production with end-to-end automation for retail or industrial formats, from bagging to palletizing.
Spices & seasonings
Help protect your product quality with clean-filling automation that minimizes cross-contamination and dust for your most sensitive spice blends.
Frozen foods
Handle frozen and IQF products with robust end-of-line automation, from retail-ready packaging to secure palletizing and pallet wrapping.
Fruits & Vegetables
For fresh, frozen, canned and bagged fruits and vegetables, we help manufacturers introduce automation designed to support food safety and consistent production.
Beverages
Improve line versatility with efficient case packing and end-of-line palletizing systems designed for a wide range of beverage container types.
Prepared foods
Scale your ready-meal and meal-kit production with high-performance case packing and palletizing that keeps your brand shelf-ready.
Food Ingredients
Ensure safe, efficient production with hygiene-first automation for high-volume powder ingredients, reducing dust and securing your supply chain.
Sauces & condiments
Utilize flexible secondary and tertiary packaging automation that supports both rigid and flexible formats, providing stable transport for your sauces.
Food & beverages packaging equipment
Bagging
Versatile systems for retail pouches to bulk formats. Precision engineered for speed, reliability, and accuracy.
Case packing
Versatile robotic systems for cases, display cases, and trays. Designed for efficiency, flexibility, and scale.
Palletizing
Reliable robotic, conventional, and cobot systems for any environment. Engineered for safety, stability, and scale.
Pallet wrapping
Turntable, rotary arm, and stretch hooder systems. Complete your line with high performance load securing technology.
Bulk handling
Comprehensive bulk handling systems and powder conveying equipment. Engineered for efficient, clean, and reliable transfer.
Conditioning, screening & mixing
Complete processing lines for organic substrates. Systems designed for precision mixing, screening, and dosing.
Peat moss field equipment
Specialized harvesting solutions with state of the art harvesters, harrows, and more for operations of any scale.
Seed & grain conditioning
Comprehensive solutions for purity, drying, and coating. Precision systems engineered to maximize yield and seed vigor.
Not sure which solution fits your needs?
Answer 5 quick questions and get instantly matched with the right equipment for your product, format and production goals.
Built for the realities of food & beverages packaging
We support the food and beverage industry with integrated automation solutions designed for safety, consistency and efficiency. Whether you are packaging products intended for human consumption or bulk food ingredients, our technologies ensure product integrity at every stage—from bagging and case packing to palletizing and pallet wrapping.
Adapted to your products
Food and beverage packaging solutions designed to handle the specific characteristics of your products—from dry ingredients to prepared meals—with consistency and care.
Designed for your formats
Automated solutions for a wide range of sizes and configurations, seamlessly supporting everything from retail-ready bagging to efficient industrial formats.
Optimized for retail-ready packaging
Solutions engineered to deliver high-quality end-of-line performance, ensuring your pouches, cases, and retail-ready packs are perfectly presented for the store shelf.
Built for product integrity
Systems engineered to protect food safety and product quality, ensuring consistency and a customer-ready presentation throughout the packaging process.
How we elevate the operations of our clients
From efficiency gains to full line transformations — real results from real partnerships.
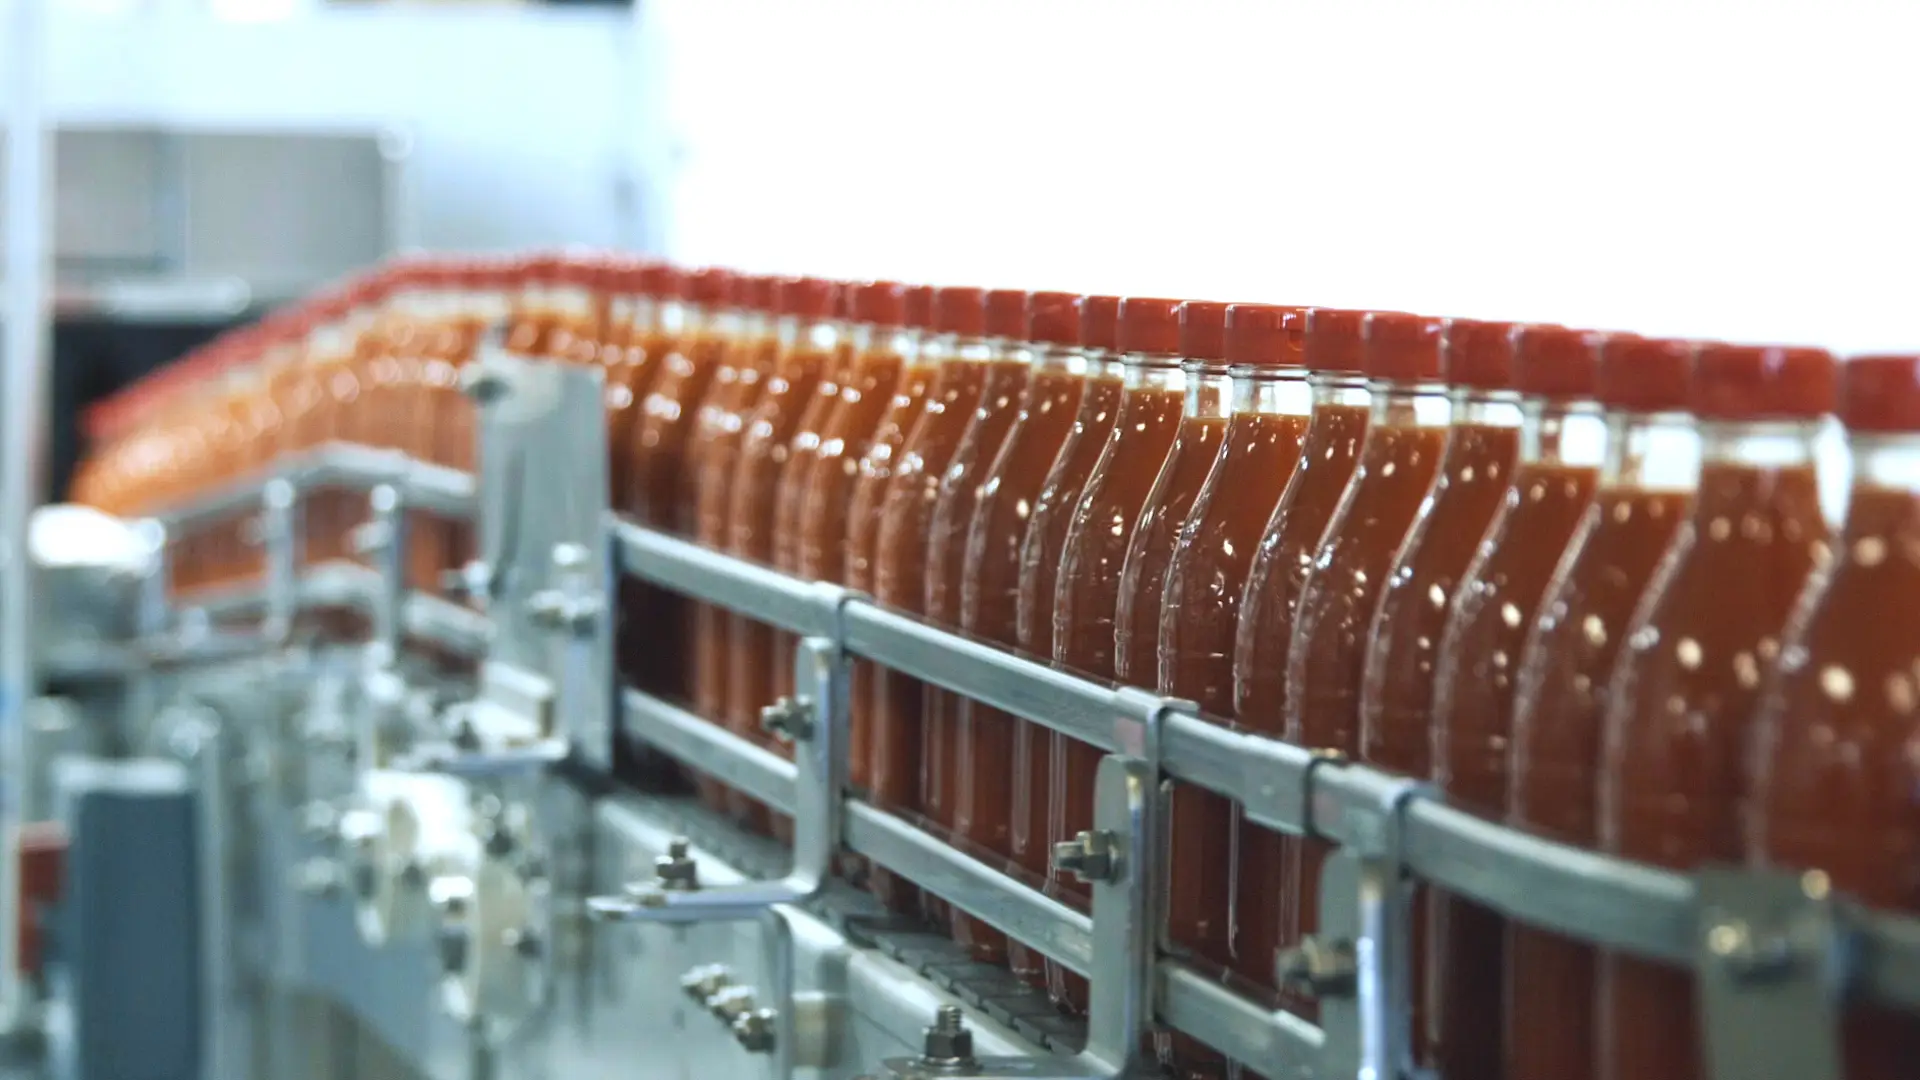
Testimonial · TW Garner
Doubling throughput for a hot sauce legend: how TW Garner transformed production with Premier Tech
2× capacity for its flagship product and a 2-year payback — how the maker of Texas Pete® automated its new sauce line from depalletizing to palletizing.
Testimonial · Maker's Mark
Blending tradition with technology: how Maker's Mark modernized palletizing
From a noisy, unreliable hydraulic palletizer to a modern, ergonomic solution — how an iconic bourbon brand eliminated team strain and daily breakdowns.
5 food packaging trends manufacturers should act on in 2026

Blog · Bagging
5 considerations when buying a bagging machine for powdery food ingredients