Packaging line automation for chemicals
Integrated, turnkey automation for the chemical industry, engineered for safe, high-precision handling of powders, granules, and complex chemical blends in intensive production environments.
Chemicals packaging equipment

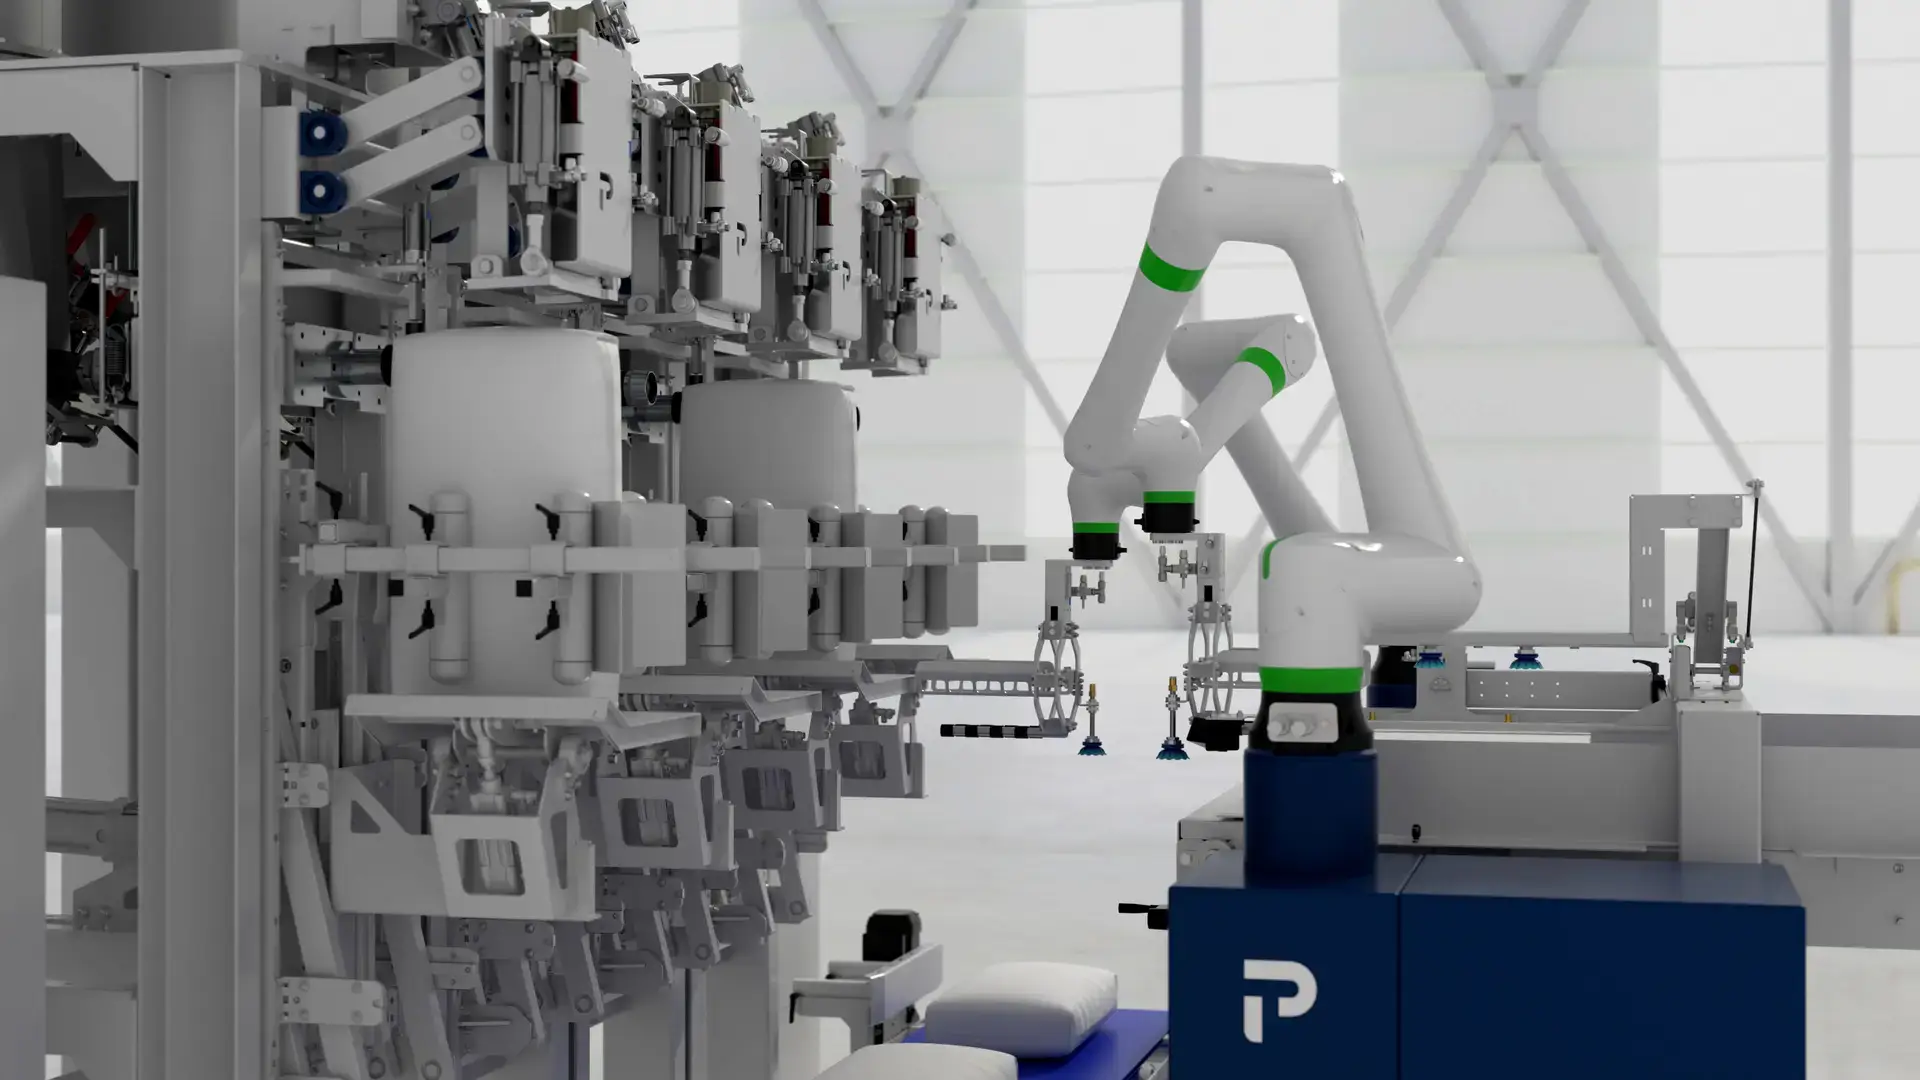
Bagging
Versatile systems for retail pouches to bulk formats. Precision engineered for speed, reliability, and accuracy.

Case packing
Versatile robotic systems for cases, display cases, and trays. Designed for efficiency, flexibility, and scale.

Palletizing
Reliable robotic, conventional, and cobot systems for any environment. Engineered for safety, stability, and scale.

Pallet wrapping
Turntable, rotary arm, and stretch hooder systems. Complete your line with high performance load securing technology.

Bulk handling
Comprehensive bulk handling systems and powder conveying equipment. Engineered for efficient, clean, and reliable transfer.

Conditioning, screening & mixing
Complete processing lines for organic substrates. Systems designed for precision mixing, screening, and dosing.

Peat moss field equipment
Specialized harvesting solutions with state of the art harvesters, harrows, and more for operations of any scale.

Seed & grain conditioning
Comprehensive solutions for purity, drying, and coating. Precision systems engineered to maximize yield and seed vigor.
Built for the realities of chemicals production
We support the chemical industry with integrated automation solutions designed for safety, consistency and efficiency. From handling complex powders, granules and additives to ensuring precise weight accuracy, our technologies are engineered to mitigate dust emission and support a clean, controlled production environment. Whether you are managing specialty chemical additives or high-volume industrial products, we help you optimize your packaging operations from industrial bagging to reliable palletizing and load stabilization.

Tailored to operational realities
Engineered to meet the specific requirements of chemical production floors, addressing strict safety standards, dust control and intensive operational workflows.

Adapted to your products
Solutions designed to handle the specific properties of chemical powders, granules and specialty products with precision and consistent material flow.

Integrated packaging line
Comprehensive packaging line automation that connects your process, from high-speed, high-precision filling to reliable palletizing and load stabilization.

Built for long-term performance
Robust, reliable systems built to endure the demanding conditions of chemical environments, delivering high-uptime performance and long-term operational value.
How we elevate the operations of our clients
From efficiency gains to full line transformations — real results from real partnerships.
Blog · Dust Control
Dust control in valve bagging: protecting your product and your people
How the right valve bagging technology minimizes dust emissions, improves workplace safety and ensures a clean, controlled production environment for chemical products.